Shearing Machine Supplier Selection Tips for Workshops That Demand Precision
2026-10-23
Ask any shop manager who’s chased a ‘bargain’ shearing machine only to watch tolerances drift: the supplier you pick can quietly make or break your precision. That’s why this guide skips the fluff and focuses on the selection criteria that actually matter for workshops that can’t afford margin creep. We’ll cover red flags, must-ask questions, and what a supplier like HUNSONE does differently when microns count.
Pin down the thinnest and thickest cuts your jobs repeat before you even pick up the phone
Start by listing every repeat action you take before dialing: checking notes, updating the CRM, pulling files, reviewing last conversation. Time each one for three days. The thin cuts are the under-a-minute tasks; the thick cuts are the ten-minute monsters. Don’t rely on memory—actual timers expose where the minutes really go.
Thick cuts deserve a hard question: does this step have to happen right before the call, or can it be batched, templated, or handed off? Often one heavy prep task turns out to be a leftover habit from a job you no longer do. Cut it or move it to a weekly block.
Thin cuts still add friction. Five quick clicks become a mental hurdle if they’re scattered across tools. Combine them into one checklist, one shortcut, or one auto-filled note. The aim is a pre-call routine that feels like a single motion, not a scavenger hunt, so you can pick up the phone faster without losing context.
Make suppliers bring their machine to your floor, or at least run your material
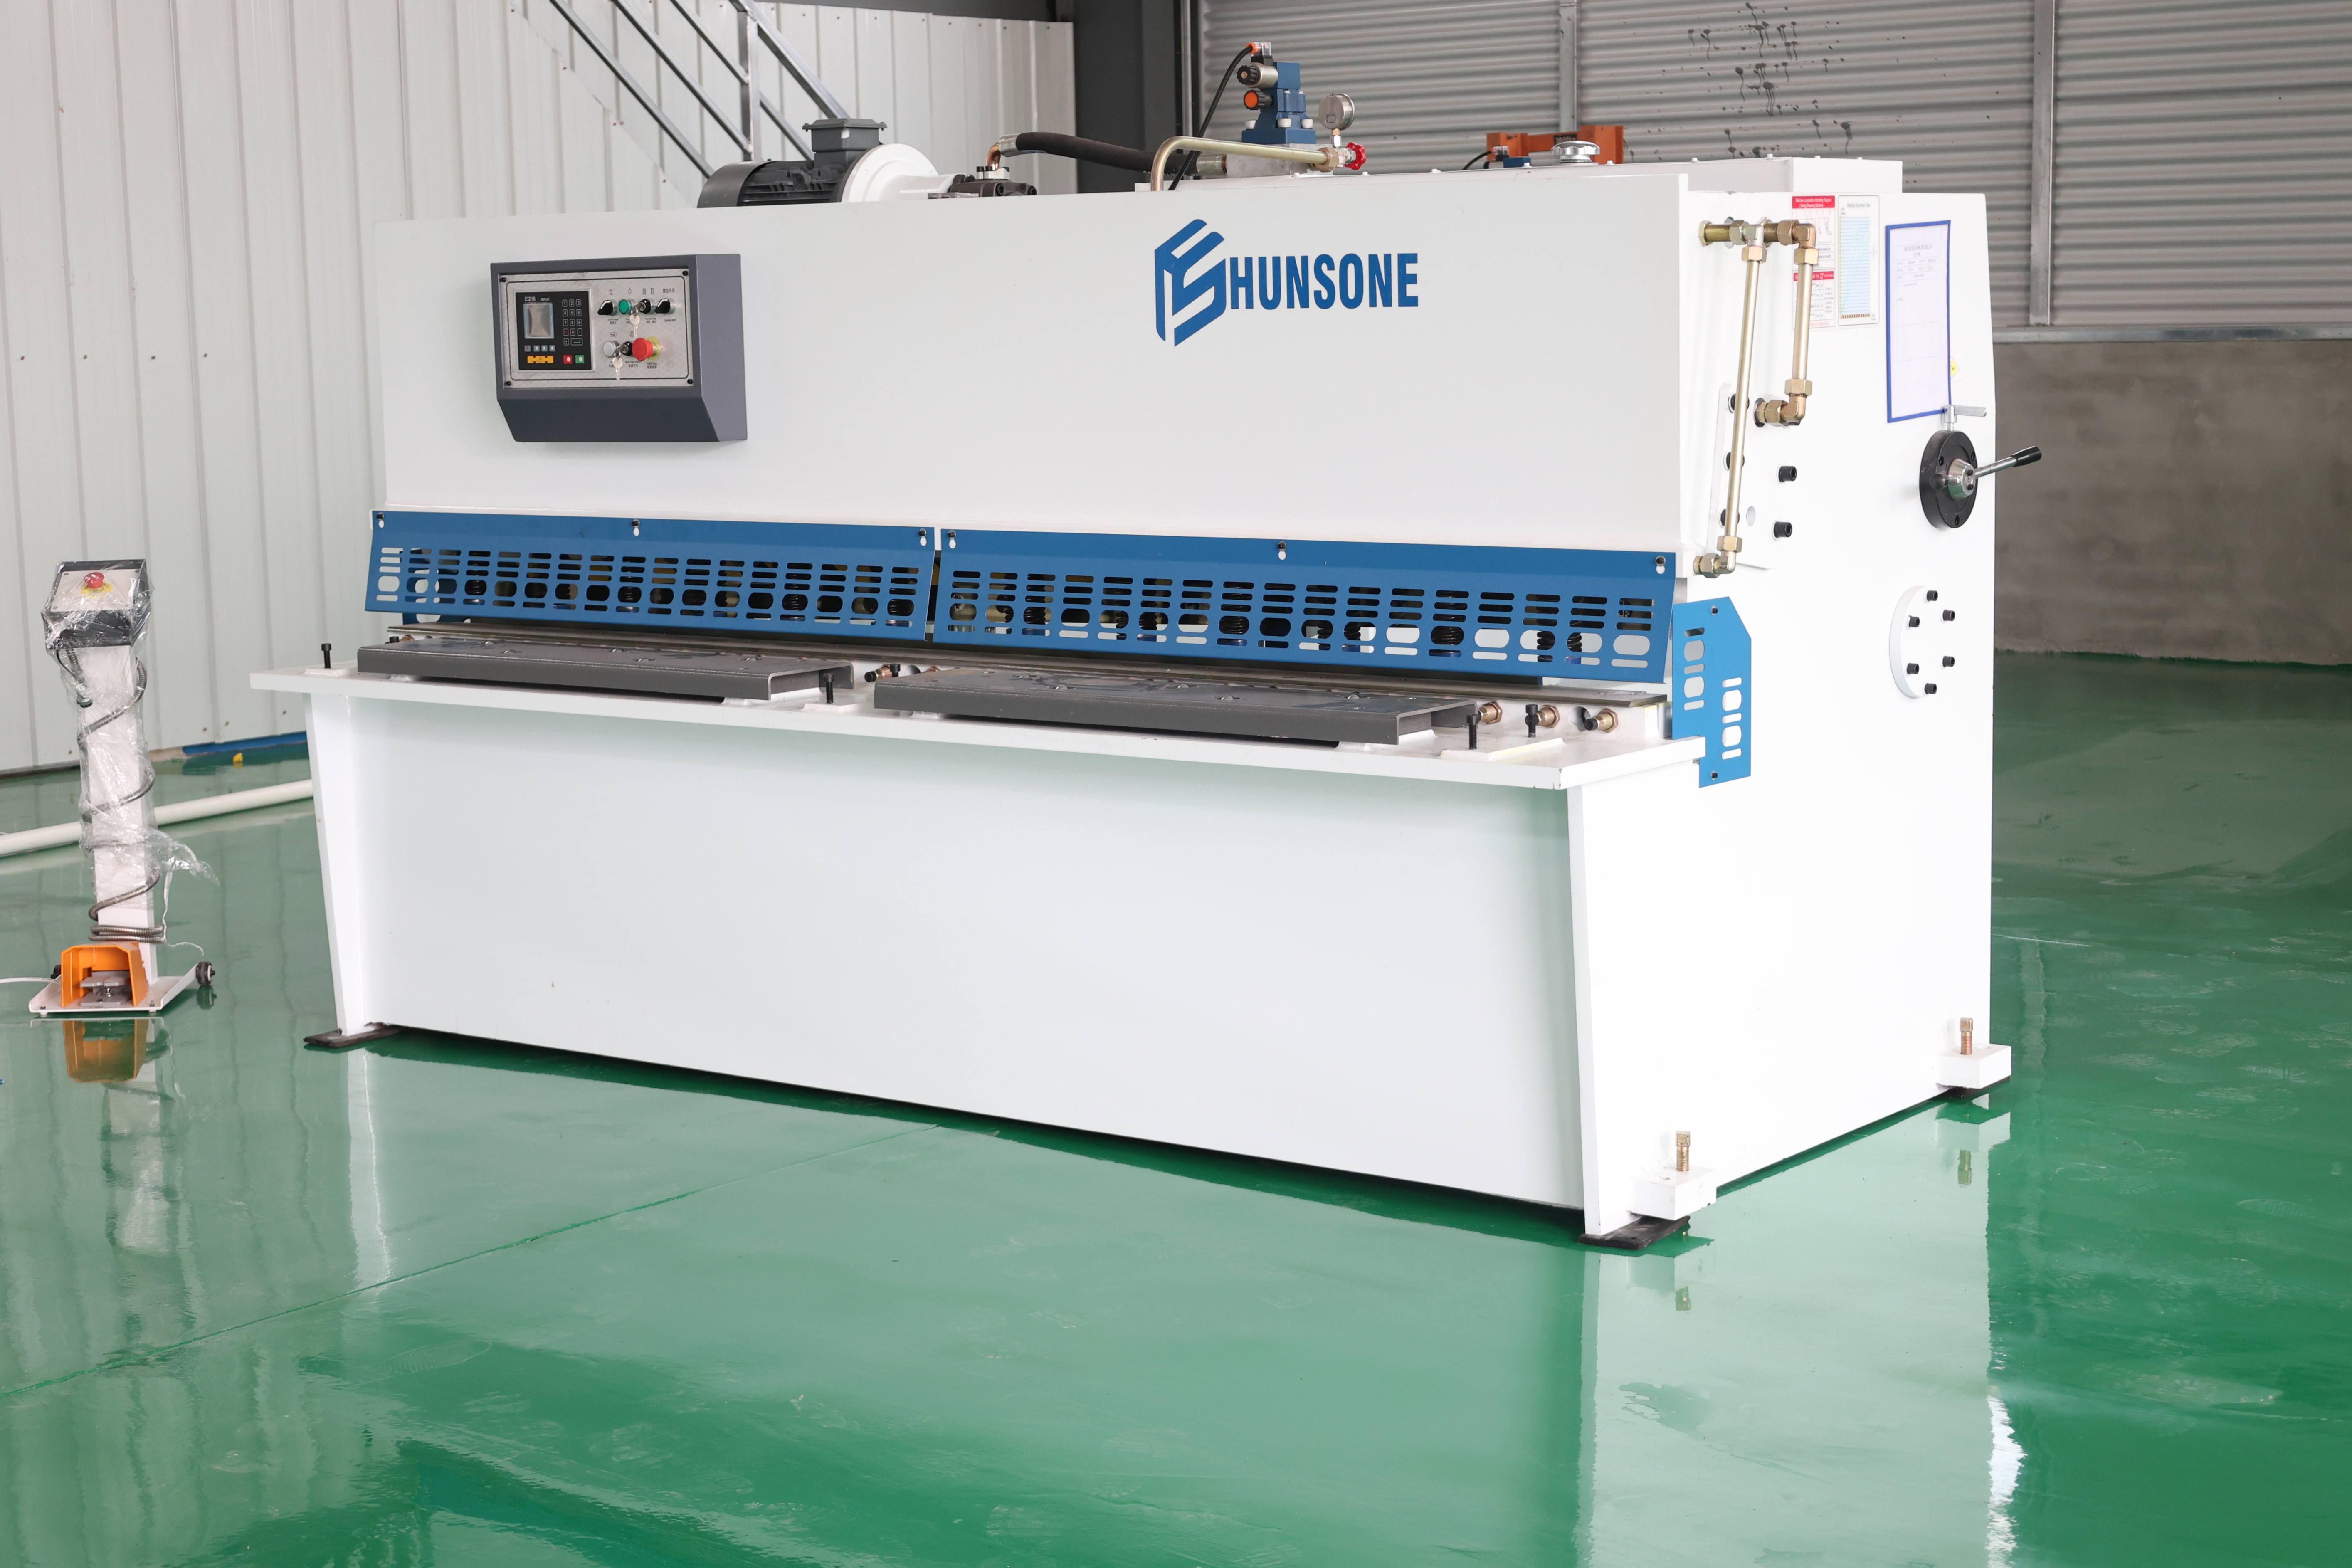
Most vendors will happily demo their equipment using the same stock they've been running for years. That tells you almost nothing about how that machine will behave with your actual parts, your fixturing, or your tolerance stack-ups. Push to have them set up in your shop, on your floor, with your operators nearby. If that's not possible, insist they run a batch of your material at their facility. The whole point is to catch the frustrations that only show up when real work hits the spindle.
Suppliers will sometimes resist because it slows down their sales cycle or exposes wrinkles they'd rather smooth over later. But the cost of finding out during production that a machine can't hold size on your particular alloy, or that chip evacuation goes sideways with your part geometry, is far higher. One shop I know forced a laser cutter vendor to run their own pre-painted aluminum sheets, and within an hour the fumes were gumming up the optics. That discovery saved them a six-figure mistake.
When you do arrange the trial, keep the scope practical. Bring a representative mix of your toughest jobs, not the easy ones. Watch for things like tool wear, thermal drift, and how much babysitting the process needs. Take notes on setup time and changeover quirks. The machine might look great in a glossy demo, but what you're buying is how it behaves on a Tuesday afternoon with your material, your deadlines, and your people leaning over the guard.
Look for a blade gap adjustment you can set without calling an engineer
Most machines hide the blade gap behind a service panel, but a surprising number of mid-range models let you tweak it with a simple thumbwheel or a pair of set screws. If you can see a small dial near the cutting head, that is probably your gap control. Turn it a few degrees at a time, run a test sheet, and watch how the cut edge changes. You will often find the sweet spot without touching a single bolt on the main assembly.
Before you reach for the phone, check whether the adjustment is meant to be user-facing. Some brands put a recessed screw under a small cover so operators can compensate for normal wear between service visits. A slight reduction in gap can stop ragged edges or paper jams, while opening it up a little helps when the blades start to bind. Mark the original position with a pencil first, and only adjust when the machine is unplugged and the blades are fully stopped.
Ask for a reference who runs the same gauge every day, not a demo video
A demo video shows a gauge under ideal conditions, with a practiced hand and fresh materials. It rarely captures the drift that shows up after a few hundred cycles, the maintenance tricks an operator learns, or the exact noise a gauge makes before it needs attention. Ask for a reference who runs the same gauge every day and can tell you what actually happens between the scheduled calibrations.
Daily operators accumulate the kind of knowledge that never makes it into a spec sheet. They can point to the one fixture that always reads high until it warms up, the cleaning routine that stops false rejections, and the setting they adjust on humid days. A real reference will describe those details in plain terms, often with a few complaints thrown in—because that honesty is more useful than a polished walkthrough.
Lock response times and spare parts into the purchase order, not the sales pitch
Too many equipment deals fall apart after the handshake. The salesperson promises a four-hour response window and a shelf of spare parts that never materializes when a line goes down. If those commitments matter to your operation, they belong in black and white on the purchase order, with penalty clauses tied to missed targets. Otherwise you're left chasing a rep who's already moved on to the next account.
A purchase order is not a formality—it's the only instrument that gives your maintenance team leverage. List the exact parts you expect to be stocked locally, the maximum time from call to arrival, and what happens if the vendor misses. Without that level of detail, "priority support" is just a phrase printed on a brochure. Make the vendor sign off on numbers they can actually deliver, not the ones that sound good in a conference room.
Real accountability shows up when a pump fails at 2 a.m. and the response time is already quantified in the contract. If the spare part isn't on the shelf, the financial consequence should be automatic, not a negotiation after the fact. That shift—from a sales pitch to an enforceable obligation—is the difference between a supplier who respects your uptime and one who just talks about it.
Work out the real cost per cut after a year of ownership, not the sticker price
People rarely track how many times they actually use a cutting tool in twelve months, which makes the sticker price a terrible way to judge value. A mower that seems cheap on the shelf can end up costing far more per session once you add fuel, oil, blade sharpening, air filters, spark plugs, and the occasional repair. The math is simple: total what you spent over the year and divide it by the number of cuts you completed. If you ran the machine forty times, a $400 mower with $120 in running costs lands at $13 per cut, while a $250 model that needed $200 in fixes and extra fuel might hit $15 or more for the same forty sessions.
The real number often surprises people because they forget the small, recurring expenses. A dull blade forces the engine to work harder, burning more fuel and wearing out belts faster. Cheap replacement parts or neglected oil changes don't show up on the receipt all at once, but they quietly push the per-cut figure higher. Tracking these costs for one full season gives you a baseline that a glossy price tag simply cannot provide.
Once you have that per-cut cost, you can compare options more honestly. A higher upfront price may be justified if it delivers lower maintenance and better fuel efficiency over hundreds of cuts. Conversely, a bargain machine that only gets used ten times a year might still be expensive per cut if it breaks down often. The goal isn't to buy the cheapest or the most expensive model; it's to understand what each actual use is costing you after twelve months of real ownership.
FAQ
Look at the supplier's track record with tight-tolerance work. Ask for examples of machines placed in similar shops and how those units held blade gap and back gauge repeatability over time, not just on day one.
It matters a lot. A rigid welded frame and a drive system that does not twist under load help keep the cut edge square. If your work involves coated or polished sheet, a supplier who can demonstrate reduced marking and consistent ram travel is worth shortlisting.
Yes, and you should shape the test around your own parts. Send the supplier samples of your typical material, thickness, and length, then require them to cut those samples while you watch. Measure straightness, burr height, and angle accuracy against your shop tolerance.
Go beyond a generic response time. Ask whether they stock critical wear parts locally, how they handle blade gap adjustment training, and whether their technicians understand high-precision sheet metal work rather than just basic installation.
Ask them about deflection compensation, rake angle adjustment for different material strengths, and how they verify back gauge positioning under load. A supplier who gives specific answers and offers test cuts usually knows the difference.
Usually yes for precision work. A heavier, well-built machine holds settings longer and reduces the chance of knife clash or wandering cuts. But confirm the extra mass is in the frame and drive, not just added ballast.
Vague claims like high precision without measurable tolerances, reluctance to provide reference shops, no clear process for factory acceptance tests, and spare parts with long lead times. Also be wary if they cannot explain how the machine maintains alignment over years of use.
Not automatically. Proximity helps with service and spare parts, but technical capability matters more. If a local supplier lacks precision-specific experience, a more distant supplier with strong remote diagnostics and fast parts shipping can be the better long-term choice.
Conclusion
Before you start calling suppliers, map the exact range of sheet thickness your shop cuts week after week—not just the occasional job, but the repeat work that pays the bills. That simple list stops you from being sold a machine that is either too light for your heaviest daily material or too rigid for your thinnest. Then insist that any serious supplier bring the machine to your floor or at least run a sample of your actual stock through it. A demo on their polished test bench with their favorite material tells you almost nothing. While it is running, ask them to set the blade gap for your thinnest gauge in front of you. If that adjustment requires a call to their engineer or a service visit, the machine will cost you hours every time you switch jobs. The gap setting is not a minor feature; it is the difference between a clean square edge and a burred, bent mess on the first cut.
References matter more than any video. Ask for a shop that runs the same gauge range you do every day, and call them when the sales rep is not on the line. Ask how the machine behaves after six months, not on day one. In the purchase order, fix the response time for breakdowns and the availability of common spare parts. A promise made during the sales pitch evaporates once the invoice is paid unless it is written with a penalty or a clear escalation path. Finally, ignore the sticker price. Add up the cost of blades, energy, downtime, rejected parts, and service calls over a full year of ownership, then divide by the number of cuts you actually make. That real cost per cut tells you which supplier respects precision, not just which one offers the cheapest crate. A machine that drifts out of tolerance or waits three days for a part will quietly eat your margin long after the discount is forgotten.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/