Piezo Ceramic Manufacturer Guide to Quality and Performance
2026-11-02
Piezo ceramic quality is often invisible until a transducer starts drifting, a sensor loses sensitivity, or an actuator cracks under cyclic load. That’s exactly when the manufacturer’s process control—not just the datasheet—proves its worth. This guide breaks down the quality and performance factors that separate reliable piezo ceramic suppliers from the rest, with practical insight from Siansonic to help you make a confident sourcing decision.
Why Powder Lot Consistency Matters More Than the Spec Sheet
A spec sheet is a snapshot, not a promise. Two lots of powder can sit comfortably within the same published ranges for particle size, flow, and chemistry, yet behave nothing alike in your machine. One lot might spread evenly and sinter predictably; the next could clump, spatter, or leave porosity in exactly the places you cannot afford to rework. When your process window is tuned to a narrow set of hidden variables—surface moisture, fines fraction, morphology—the broad tolerances on a data sheet offer almost no protection.
Real production problems rarely show up as an out-of-spec number. They show up as a 2% drop in density, a sudden need to tweak laser power, or a batch of parts that pass inspection but fail in the field. That is where lot consistency earns its keep. A supplier that controls the upstream feedstock, milling parameters, and blending protocol gives you the same powder every time, so your validated recipe stays valid. Chasing the cheapest spec-sheet match often means inheriting someone else's process variation.
Lot-to-lot drift also has a compounding cost. Every time you adjust settings to accommodate a new lot, you burn machine hours, operator attention, and material. Over a year, those small resets add up to more than the price difference between a consistent lot and a cheap one. The spec sheet tells you what the powder might be; lot consistency tells you what it will be, order after order.
Sintering Profiles Are Where Piezo Ceramic Manufacturers Cut Corners
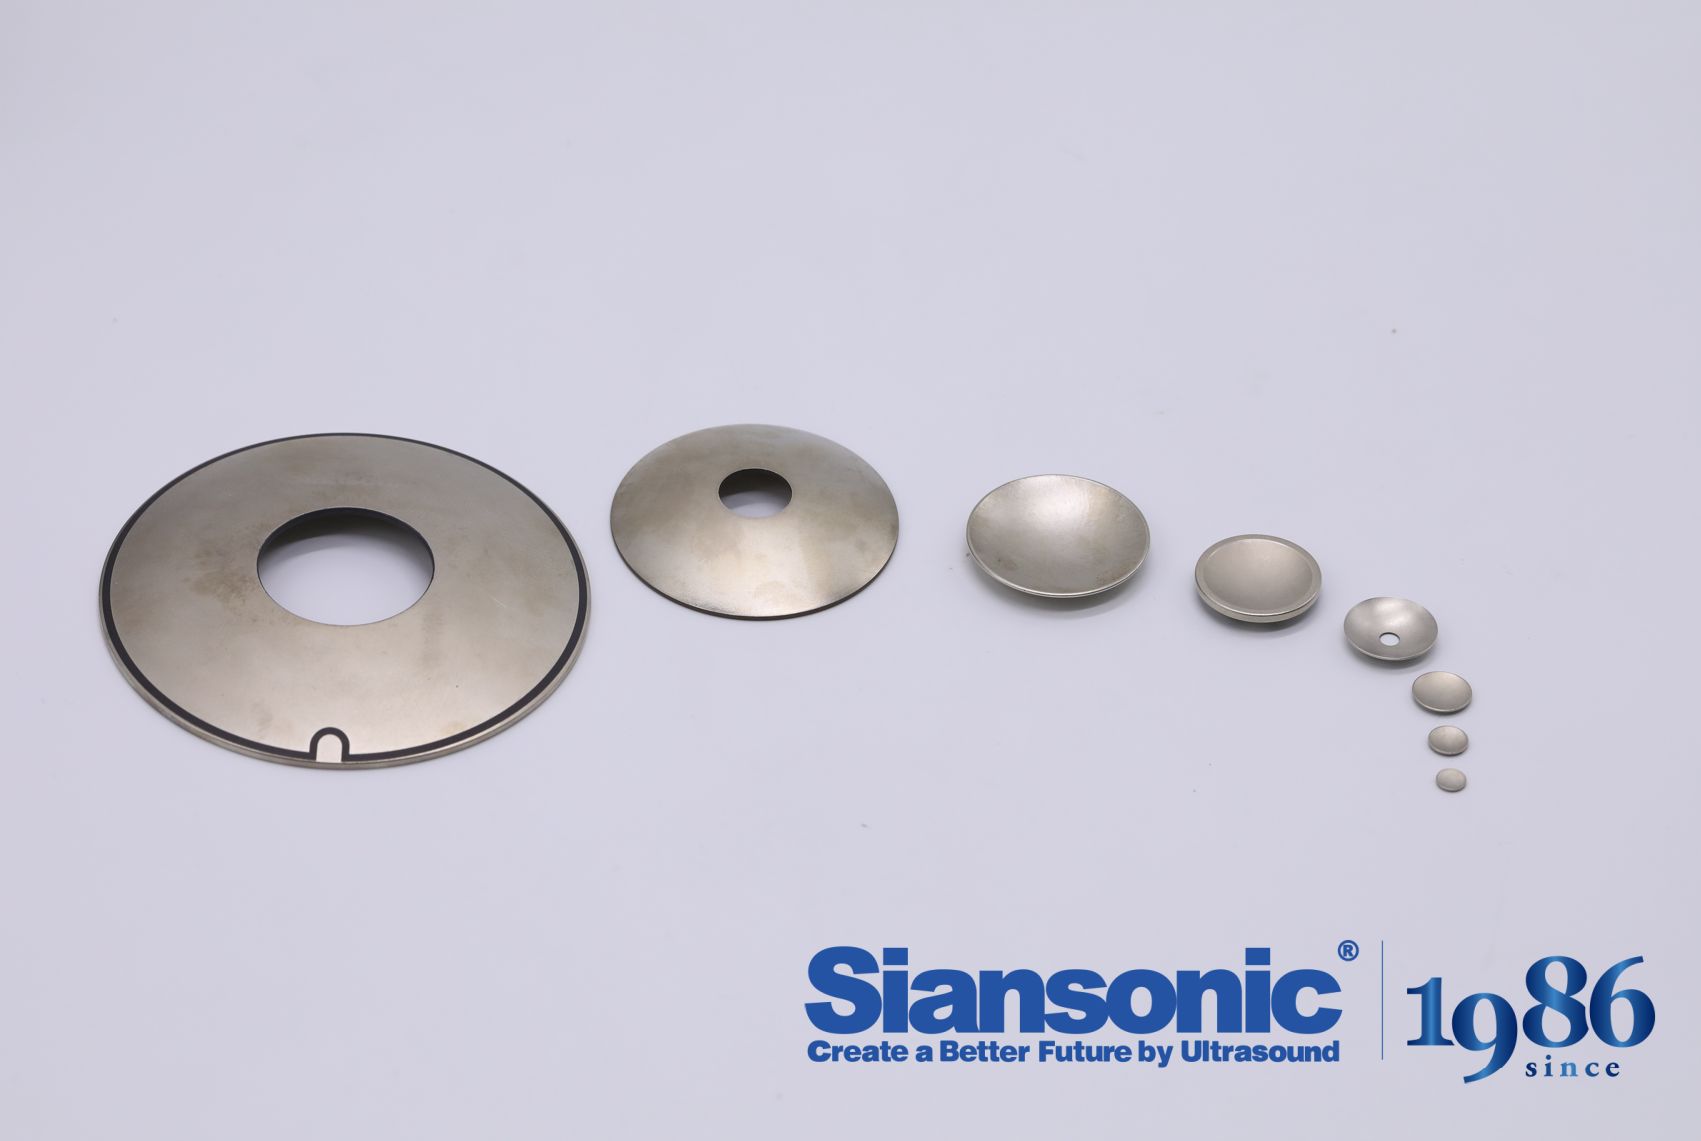
When a piezo ceramic element fails prematurely or delivers inconsistent output, the root cause rarely lies in the raw powder. More often, it traces back to the kiln. Sintering is where the material's crystalline structure locks into place, and even small deviations in ramp rates, dwell time, or cooling curves can leave behind residual stress, microcracks, or uneven grain growth. Some manufacturers shorten the high-temperature soak to push more batches through, but that shortcut shows up later as reduced coupling coefficients, higher dielectric loss, or parts that drift out of spec after a few hundred cycles.
The corners get cut in subtle ways: a faster ramp up to save energy, a slightly lower peak temperature to protect the furnace elements, or an accelerated cooling phase that skips the annealing step. These choices are rarely visible on a datasheet. The element may look identical, pass a basic capacitance check, and even meet initial displacement targets. But without a properly controlled sintering profile, the poling process becomes less effective, and the long-term stability of the part suffers. You end up with transducers that lose sensitivity after a few months in the field or actuators that need higher drive voltages to produce the same motion.
Quality-conscious piezo manufacturers treat the sintering profile as a proprietary recipe, not a generic cycle. They monitor atmosphere, control temperature uniformity across the entire batch, and validate each lot with impedance analysis rather than simple dimensional checks. If a supplier cannot explain what happens inside their kiln between 800°C and 1300°C, that is a strong signal the corners are being cut somewhere in the thermal process, even when the paperwork says otherwise.
Electrode Choices That Change Behavior Under Load
Selecting an electrode isn't solely about rated capacity. Under sustained load, the kinetic profile takes over. Graphite anodes that maintain a tidy voltage curve at 0.2C can sag badly at 5C because lithium ions pile up at the particle surface and fail to intercalate fast enough. Swapping in a hard carbon or adding a modest silicon fraction shifts the onset of lithium plating to higher currents, but it also changes the voltage window, so the safe state-of-charge limit has to move accordingly.
Cathode choice matters just as much when the current density jumps. LFP's flat plateau can hide localized overpotentials until the terminal voltage drops suddenly, giving operators less warning. Nickel-rich NMC, by contrast, shows a more gradual decline, but repeated high-rate pulses tend to crack its polycrystalline secondary particles. Switching to single-crystal morphologies or blending a small amount of LMFP keeps the impedance rise in check without sacrificing the early-warning slope.
The mechanical and electrical scaffolding around the active material often determines whether high-rate behavior is reversible. Replacing PVDF with a waterborne binder can cut ionic resistance, yet the coating may lose adhesion as particles swell. A hybrid conductive additive, short carbon nanotubes bridging larger carbon black clusters, preserves electron pathways even when the electrode expands. Porosity needs the same attention: a narrow distribution around 200–400 nm allows fast ion transport while avoiding the dead volume that drags down volumetric energy density.
Poling Field Uniformity Separates a d33 of 400 from 650
The gap between a d33 of 400 and 650 pC/N often comes down to something easily overlooked: how evenly the poling field reaches every volume of the ceramic. Most laboratories report the nominal field strength as voltage divided by thickness, but that number says little about local intensity near edges, voids, or electrode imperfections. A nominally poled disk can have a saturated rim, a partially switched core, and dead zones around micro-voids. The measured coefficient is then a spatial average that hides this inconsistency and lands closer to 400.
Nonuniformity also creates a hidden stability problem. Under-poled regions retain more randomly oriented domains, which makes the material more prone to aging and depoling under thermal or mechanical stress. In contrast, when the field profile is smoothed out—by rounding electrode edges, submerging the sample in an insulating fluid, or applying multiple short pulses instead of one long ramp—the domains switch in a more synchronized manner. The same ceramic that once averaged 400 pC/N can then reach the 650 pC/N range without any change in composition.
This distinction matters because it reframes d33 as a process metric rather than a fixed material constant. A low value may not indicate a bad formulation; it may simply reveal that the poling setup never gave the material a fair chance. Engineers who chase higher coefficients by reformulating the ceramic while ignoring field uniformity are often leaving 200 pC/N or more on the table.
Mechanical Q Factor Tests Reveal How Much Energy Is Actually Lost
When a structure rings after being struck, the decay rate of that vibration tells you more than just how lively the material feels. Mechanical Q factor measurements track this decay cycle by cycle, and each drop in amplitude corresponds to a fraction of the stored elastic energy being dissipated as heat, internal friction, or acoustic radiation. The tests don't measure a single loss mechanism in isolation—they capture the combined effect of every microscopic slip, dislocation movement, and boundary interaction that quietly drains energy from the system.
What makes the Q factor so revealing is that it relates stored energy to energy lost per cycle through a simple ratio. A high Q means the system holds onto most of its energy from one oscillation to the next; a low Q means a significant portion is gone before the next swing begins. In practice, test engineers track the logarithmic decrement of free vibration or the width of a resonance peak under forced excitation, and both routes expose the same underlying loss picture. The energy isn't destroyed—it ends up as heat at grain boundaries, as motion at micro-cracks, or as sound leaking into surrounding air.
These measurements become especially useful when comparing nominally identical parts. Two samples can look identical on a drawing and still show very different Q values because small differences in porosity, residual stress, or surface finish alter how much energy escapes per cycle. By running repeated tests across frequency and amplitude, you can separate linear damping from amplitude-dependent losses, pinpoint the dominant dissipation mechanism, and make informed decisions about material selection or heat treatment.
Burn-In Tests Expose the Gap Between Lab Results and Field Performance
Burn-in tests have a way of shattering the tidy assumptions made in controlled environments. A component that sails through accelerated life testing on a bench can stumble within weeks of actual deployment, where thermal cycling, humidity swings, and unpredictable load patterns conspire in ways no lab protocol fully replicates. Engineers often discover that the failure rate during early field use tracks closer to a bathtub curve's sharp left edge than the optimistic projections derived from pristine test chambers.
The discrepancy isn't merely statistical noise—it's a structural blind spot. Lab setups tend to isolate stressors, applying them one at a time or in fixed sequences. Real-world conditions, however, layer vibration on top of temperature extremes, add voltage transients from nearby equipment, and introduce contaminants that accumulate gradually. Burn-in tests, when designed with field telemetry in mind, expose these compounding effects. Without that reality check, a product can ship with latent weaknesses that only surface when a technician is already on site, turning a routine installation into an extended debugging session.
What makes the gap both frustrating and instructive is that it changes across product generations. A capacitor that held up fine in the previous design might fail prematurely once a new firmware update pushes duty cycles higher. Burn-in programs that feed field failure data back into the test profile help close that loop, but only if teams treat the test not as a gatekeeping formality but as a living map of where lab confidence ends and operational truth begins.
FAQ
A supplier worth trusting will talk openly about batch-to-batch variation, raw material sourcing, and polarization stability. If they only quote price and lead time without asking about your operating frequency, load, or temperature swings, that is a warning sign.
It depends on whether you are sensing or driving. For sensors, look closely at d33 and g33. For actuators, d33 and strain hysteresis matter more. Always check the coupling factor and mechanical quality factor against your bandwidth needs, not just the headline constants.
Silver electrodes are common but can migrate under high DC fields and humidity. Nickel offers better resistance in some environments, while gold is preferred for demanding micro-actuators. The adhesion layer and edge coverage often matter just as much as the electrode metal itself.
Fatigue is rarely from the ceramic itself. Usually it is microcracks starting at electrode edges, depolarization from repeated thermal stress, or bonding layer degradation. Good manufacturers mitigate this through dopant choices, controlled grain size, and clean edge termination.
At minimum, impedance spectrum, capacitance and dielectric loss, d33 measurement, and dimensional checks. For high-reliability parts, ask for resonant frequency distribution and microscopic inspection of electrode coverage. Batch traceability to raw powder lots is also a basic expectation.
Yes, but only with careful tooling and polarization fixturing. The risk comes from non-uniform poling in irregular geometries or stress concentration in sharp corners. A capable maker will adjust electrode patterns and poling conditions rather than simply machining a standard block to size.
Every material has a Curie point and a safe working range well below it. Approaching that limit causes irreversible depolarization. Also watch the temperature coefficient of capacitance and resonance frequency drift if your control loop depends on stable impedance.
Vague test data, reluctance to share failure analysis, no material traceability, and quoting only generic PZT-5H or PZT-4 without discussing dopant levels. If they accept an order without asking about drive level, duty cycle, or environmental exposure, expect surprises later.
Conclusion
A piezo ceramic's datasheet can look flawless while the material itself behaves nothing like it in a real transducer. The first place that drift starts is the powder. Two lots from the same supplier can share an identical chemical formula and still differ in particle size distribution, impurity levels, and surface reactivity. Those differences survive calcination and get baked into the grain structure, so a manufacturer that treats powder lots as interchangeable is already compromising repeatability before a single disc is pressed. Sintering makes it worse. A tight, well-characterized profile controls grain growth, density, and the ratio of tetragonal to rhombohedral phases near the morphotropic boundary, but short cycles and uneven kiln loading save cost at the expense of internal stress and microcracks. Electrode application then decides how the part behaves under load. Silver paste may be fine for a low-duty buzzer, but high-field or high-cycle applications often need fired-on nickel or silver-palladium with matching thermal expansion, otherwise the electrode delaminates and the effective coupling drops.
Poling is where the real d33 numbers are made or lost. A uniform field across the full electrode area, held long enough and at the right temperature, pushes domain alignment from a mediocre 400 pC/N toward 650 pC/N; a poorly fixtured poling rig creates edge effects and leaves the center only partially switched. Mechanical Q testing then reveals how much of that performance survives as useful motion. Low Q means the material dissipates energy as heat, which is acceptable for broadband sensors but fatal for resonant actuators and ultrasonic welders. Finally, burn-in tests close the gap between lab coupons and field reality. Subjecting finished parts to temperature cycles, voltage load, and mechanical pre-stress for 48 to 100 hours separates stable products from those that fade after a week in a customer's machine. A manufacturer that controls all six steps will deliver ceramics that hold their d33, Q, and capacitance over time, not just on the first incoming inspection report.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/