OEM Leather Rivets Guide to Sourcing Quality Hardware for Leather Goods
2026-11-02
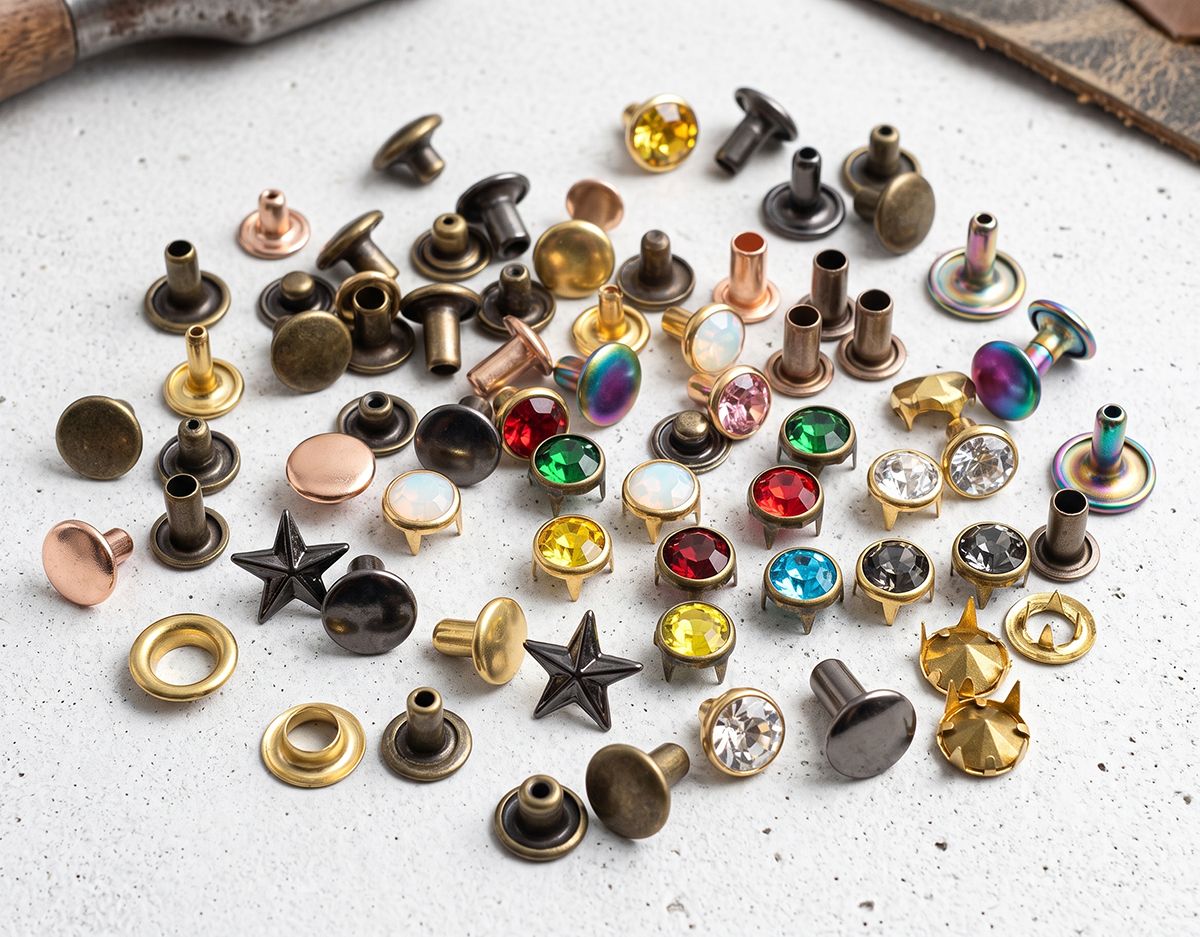
Nothing undermines a beautifully finished leather piece faster than hardware that gives out too soon. For makers and brands, finding OEM leather rivets that balance strength, finish consistency, and cost is rarely as straightforward as it should be. This guide cuts through the guesswork, covering what actually matters when sourcing rivets for leather goods. Along the way, you’ll see why many workshops now turn to Kingming for rivets that hold up in daily use.
Rivet Material Choices That Hold Up in Daily Use
Daily wear has a way of exposing weak rivet choices faster than any spec sheet. On a pair of jeans, copper rivets develop a dark patina from sweat and detergent, and that layer actually shields the metal underneath; swap in plain steel and the rivet shank will rust through the seam within months. Stainless isn’t a one-size-fits-all answer—304 can show pitting in coastal air, while 316’s molybdenum content makes it far more resistant to chloride, which is why it shows up on backpack buckles and outdoor gear.
Aluminum rivets keep weight down, but their shear strength is roughly a third of steel’s, so they’ll deform or snap in high-stress spots like a luggage handle pivot or the hinge pin on a folding knife. Steel rivets are tough, yet the finish does most of the work: black oxide or zinc plating can double corrosion resistance, but once the coating gets scratched, the exposed area starts rusting fast. Titanium splits the difference—about half the weight of steel with near-steel strength—and it barely reacts with sweat, which has made it a favorite on high-end knives and EDC tools, though the machining cost can push the price up by an order of magnitude.
When two different metals meet at a rivet joint, galvanic corrosion becomes the quiet killer. An aluminum rivet set into a stainless steel plate will act as the anode and sacrifice itself in rain or salt spray, sometimes losing its head in a few months. A nylon washer or a closer match in electrochemical potential can slow that down, and small-batch field testing under real daily conditions often tells you more than a lab salt-spray chart.
Reading OEM Supplier Capabilities Before You Commit
Many companies sign an OEM agreement after a single polished sales pitch, only to discover later that the supplier’s real production floor bears little resemblance to the brochure. Before you commit, ask for a walk through their current lines—not a curated tour, but an unscripted look at how they handle changeovers, bottlenecks, and rework. Pay attention to whether operators follow work instructions or rely on tribal knowledge, because that tells you more than any capacity chart.
Capability isn't just about machine lists or ISO certificates on the wall. It shows up in how the supplier manages tolerances, supplier sub-tier quality, and design-for-manufacturing feedback. Request a sample run of a part that is similar to your toughest geometry, and watch how their engineers communicate issues. A capable OEM partner will flag risks early instead of waiting for your inspection to catch them. Also check their recent project mix—if they’ve been making the same three components for five years, their flexibility may be limited.
Finally, look at how they handle non-conformance and corrective actions. Every factory has defects; the difference is whether they own them quickly and trace root cause, or just sort and ship. Ask to see a CAPA report from the last quarter and talk to the quality manager directly. If the answers are vague or defensive, that hesitation is a capability signal in itself. Commit only when the evidence on the floor, in their data, and in their people all point the same direction.
Custom Rivet Finishes That Resist Wear and Corrosion
When standard rivets fail too soon, the problem usually isn't the fastener itself—it's the finish. Salt spray, constant friction, and chemical exposure chew through ordinary coatings in months, leaving behind rust blooms and loose joints. Custom rivet finishes take a different route. Instead of relying on a generic layer of zinc or nickel, we adjust the plating thickness, choose alloys that match the actual environment, and sometimes add a passivation layer that seals micro-pores before they become corrosion sites. The result is a surface that holds up under repeated load cycles and still looks clean after years outdoors.
Wear resistance comes from more than hardness. A rivet that gets installed and then sits static doesn't need the same finish as one that rubs against a moving bracket every day. For high-friction applications, we often use a duplex coating—a thin, hard underlayer like electroless nickel topped with a dry-film lubricant. That combination cuts galling during installation and slows abrasive wear in service. The trick is matching the finish to the failure mode you're actually seeing, not just adding more thickness.
Corrosion is trickier because it rarely attacks evenly. A rivet head might look fine while the shank is quietly losing material inside the hole. Custom finishes let us target those hidden zones, whether that means a thicker deposit near the shear plane or a chromate conversion coating that creeps into tight clearances. We also test with the exact mating materials—mixing stainless rivets with aluminum sheet can create galvanic couples that eat through standard finishes fast. By adjusting the coating stack and sealing edges, the rivet becomes the last part to fail, not the first.
Tolerance Checks That Separate Reliable Hardware from Rejects
A tolerance check isn't some bureaucratic checkpoint—it's the moment a machined part earns its place. The reliable units pass not because they look right, but because every critical dimension falls inside a band that accounts for thermal drift, tool wear, and measurement noise. Anything outside that band gets pulled, not argued with.
What separates dependable hardware from the reject pile is how those checks are designed. Go/no-go gauges catch gross errors fast, but real confidence comes from variable data such as roundness, flatness, position, and runout read against upper and lower limits tied to actual assembly stress. If a batch drifts toward the edge of tolerance, the process gets adjusted before parts start failing downstream. That's the difference between shipping a component and shipping a problem.
Negotiating Bulk Orders Without Sacrificing Rivet Integrity
When you're sitting across from a supplier and pushing for a lower per-unit price on ten thousand rivets, it's tempting to treat the fastener as a commodity. But the moment you negotiate purely on cost, you risk opening the door to substitutions: a softer alloy, a thinner shank, a sloppier heat treatment. The first rule is to make integrity non-negotiable in writing. Specify the exact material grade, tensile strength, shear capacity, and plating thickness in your RFQ. If the supplier knows you'll run incoming inspection with a hardness tester and a micrometer, they won't offer a downgraded version just to hit your target price.
Volume leverage works best when it's tied to process efficiency rather than material compromise. Ask for a breakdown of the quote: raw material, forming, heat treatment, plating, packaging. Often you can cut 5 to 8 percent by adjusting packaging from individual boxes to bulk-line feed containers, or by agreeing to longer lead times that let the supplier batch your order with others. You can also negotiate annual volume tiers with a rebate structure—commit to 200,000 rivets over twelve months, and the supplier may trim the unit cost while keeping the same certified lot traceability. Never accept a price cut that comes without a documented change to the manufacturing route; that's where integrity bleeds away.
Finally, build a small audit into the negotiation itself. Insist on a first-article inspection report from an independent lab before the bulk run, and require periodic lot samples during production. This isn't about distrust; it's about signaling that rivet integrity is a measured specification, not a vague promise. Suppliers who push back on independent verification are often the ones banking on your incoming inspection being too slow or too shallow. When you hold the line on metallurgy and dimensional checks, you'll find that the real negotiation shifts from price to total cost of ownership—and you'll pay less per reliable rivet, not per rivet-shaped object.
From Sample Approval to Consistent Production Runs
Sample approval often feels like the finish line, but it’s really just the starting block. The swatch that earned a nod in the showroom can behave very differently once it hits the production floor. Thread tension, dye lot variations, and machine calibration all shift once you move from a single artisan piece to a run of five hundred. The real work begins when you translate that approved sample into a repeatable process that doesn’t rely on luck or a particular operator’s touch.
Bridging that gap takes more than a spec sheet. You need a clear handoff: detailed construction notes, approved trims, exact measurements, and a tolerance range that respects both the material and the method. It helps to run a small pilot batch first—maybe a dozen units—to catch the inconsistencies that only show up when fabric is cut in layers and seams are assembled under time pressure. Adjust the pattern, tweak the workflow, and document every change in a way that a new team member could follow without asking.
Once the pilot is dialed in, consistency comes from routine, not heroics. Standardize the critical steps, keep reference samples at each station, and schedule spot checks at intervals that catch drift early. Production runs rarely fail all at once; they fray at the edges—a skipped pressing step, a dulled blade, a vendor substitution. The goal isn’t to prevent every possible issue, but to build a system where good output becomes the default, not the exception.
FAQ
Durability comes down to the shank-to-cap connection and the metal alloy. A solid brass or copper rivet with a peened shank will rarely loosen, while a hollow tubular rivet with a thin plating may crack when the leather flexes. For anything that bears weight, choose a rivet where the cap and shank are formed from one piece rather than welded together, and ask the factory for a bend test video before bulk production.
Measure the total thickness of all layers being fastened, then add about 2 to 3 mm for the clinch allowance. Too little and the rivet will not roll over properly; too much and you get a loose, lopsided set. If your leather varies within the same product line, order two or three shank lengths and do a small pilot run to match each stack-up.
Watch for inconsistent shank diameters, which cause some rivets to set perfectly and others to split the leather. Poorly tumbled rivets may have sharp burrs that scratch the hide during setting. Another red flag is uneven plating that wears off after a few dozen open-and-close cycles, leaving a dull gray patch on the cap.
Many low quotes use a thin brass plating over steel or zinc, not solid brass. The base metal drives cost far more than the plating. Also, lower-grade factories may skip the final polishing and sorting steps, which means you receive mixed batches with cosmetic defects. Get a material composition certificate and ask for the actual brass percentage, not just 'brass finish.'
Specify the cap diameter, cap height, shank diameter, overall length, and the exact curvature of the cap top. Include a cross-section sketch showing whether the shank is solid or tubular. Note the finish required, such as antique brass or nickel, and give a tolerance range for each dimension—usually ±0.1 mm for the shank and ±0.2 mm for the cap. If you leave out tolerances, the factory will use its own loose standard.
Ask the supplier to keep a master sample from the first approved batch and reference it on every new purchase order. Insist that the plating bath and polishing wheel grit remain unchanged between runs. A sudden shift in color usually means the factory switched plating vendors or changed the tumbling time, so require a pre-production sample for each repeat order even if the design is unchanged.
For fully custom tooling, most factories set a minimum around 5,000 to 10,000 pieces per size because they need to run a dedicated machine cycle. Smaller brands can group several sizes or finishes into one order to reach the minimum, or choose a semi-custom option where the factory modifies an existing cap shape. Be cautious of suppliers offering very low minimums with no tooling fee—you will often pay for it through a much higher unit price.
Conclusion
Sourcing OEM leather rivets for leather goods isn't just about picking a metal pin—it's about matching the hardware to how the product will actually be used. Brass and copper offer classic looks and decent corrosion resistance, but coated steel or solid stainless might be better for bags and belts that face daily friction and moisture. Before you place any order, dig into the supplier's actual capabilities. Ask for their tolerance data, not just a glossy catalog. A rivet that's off by a fraction of a millimeter may look fine in a sample but will cause loose posts, cracked leather, or returns down the line. The best OEM partners will show you their inspection reports and let you set acceptable deviation ranges.
Finish quality matters just as much as base metal. Look for electroplating or powder coating that has passed salt-spray and abrasion testing—otherwise that antique brass look can rub off within weeks. When you negotiate bulk pricing, don't let cost per piece erode the specs you approved. Keep the same alloy, plating thickness, and post dimensions; if the supplier wants to swap materials, demand a new sample run and test batch. Lock down a clear approval process: from first article samples to pilot production, every stage should have measurable pass/fail criteria. That way, the rivets in your 5,000-unit order match the ones you inspected, not a downgraded version.
Contact Us
Contact Person: Jamie Zeng
Email: [email protected]
Tel/WhatsApp: +86 13728219269
Website: https://www.kmhardware.com