Corrugated Rotary Die Making Equipment Factory Precision Engineering Explained
2026-11-02
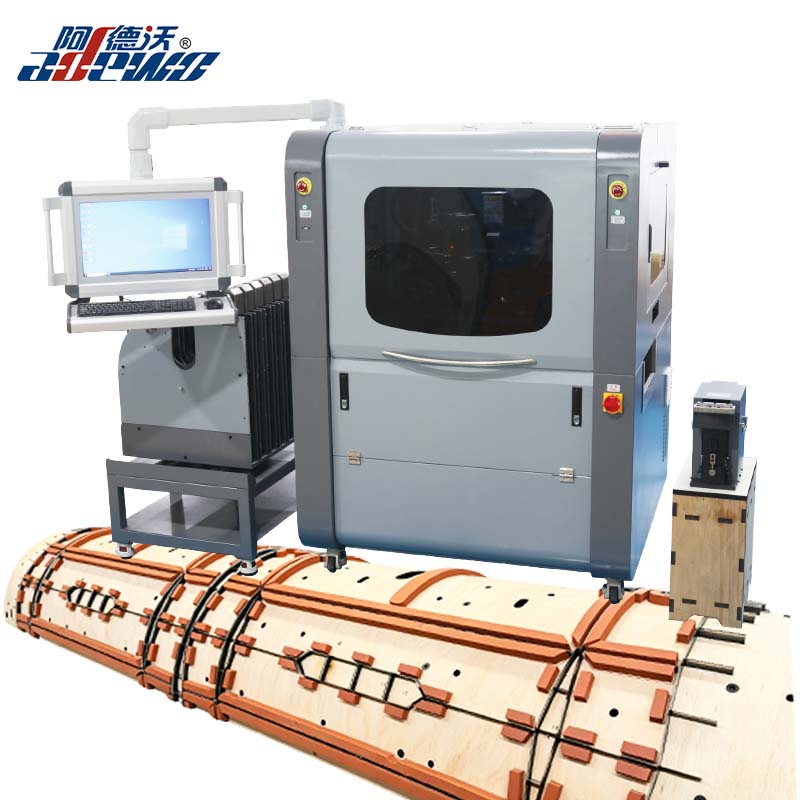
Ask any corrugated converter what keeps them up at night, and rotary die cutting accuracy will top the list. A fraction of a millimeter off, and a full production run turns into scrap. That’s where precision engineering stops being a buzzword and starts living on the factory floor—specifically at ADEWO, a manufacturer that builds rotary die making equipment around one uncompromising principle: every cut must be repeatable, every roller must stay true. In this post, we’re opening the doors to that factory, showing how raw steel, CNC machining, and hands-on assembly come together to produce tooling that holds tolerances others only promise.
The Steel Choice That Keeps Edges Sharp Past the Expected Run
Blades dull when their microstructure breaks down under repeated stress. Most steels trade hardness for toughness, leaving you with an edge that folds or chips before its time. The alloy behind this knife leans into a different balance: fine vanadium carbides sit densely in the matrix, acting like microscopic teeth that resist deformation without turning brittle.
What you notice in daily use is the absence of that mid-shift fade. Where a typical kitchen knife demands steeling after a couple of prep sessions, this one keeps slicing tomatoes cleanly past the point you would normally reach for a honing rod. The edge retention comes not from a thicker grind, but from carbides that stay anchored as the surrounding steel wears away slowly and evenly.
Sharpening, when it finally arrives, feels different too. Instead of fighting a gummy edge that rolls over, you are refreshing a crisp apex. A few light passes on a fine stone bring back the bite, because the steel has not collapsed into itself. That is the real payoff: fewer interruptions mid-task, and an edge that still cuts the way it did on day one, well beyond the expected run.
Micron-Level Tolerances You Can Hear in a Quieter Cut
You hear a cheap blade before you see the burn marks. The whine, the rattle, the way the pitch jumps when the stock gets hard—those sounds come from runout and uneven tooth engagement measured in microns. On a well-built arbor and a properly tensioned plate, that noise doesn't disappear by accident. It's engineered out by holding bearing journals, flange faces, and tooth geometry to tolerances most shops can't measure without a laser.
The quiet shows up in other ways too. A blade that tracks within a few microns spreads the cutting load evenly across every tooth, so the edge doesn't slam and skip. There's less heat, fewer sparks, and the motor keeps a steadier note instead of surging. You feel it as much as you hear it—a smoother feed, a straighter line, and a cut surface that needs almost no sanding before finish.
This is the difference between making a blade and making it right. The specs don't shout. They sit in the background, holding every part in a relationship close enough that nothing rubs, slaps, or chatters. When the tolerances finally stack up in your favor, the saw itself seems to take a breath. The cut gets quieter because there's simply less chaos happening at the edge.
Balancing Mass and Speed for Vibration-Free Rotation
In a rotating assembly, uneven mass distribution is rarely visible to the eye but shows up quickly as vibration once the shaft starts spinning. Even a few grams placed off-center on a large flywheel can generate a noticeable oscillating force, especially as rotational speed climbs. That force grows with the square of the speed, which is why a component that feels smooth at a few hundred RPM may shake violently at several thousand. Balancing therefore begins with measuring where the heavy spots are and correcting them, not just making the part statically level.
Speed introduces a second variable that mass correction alone cannot always solve. Every rotor has natural frequencies, often called critical speeds, where residual imbalance aligns with the shaft's own bending modes. Passing through a critical speed too slowly gives the vibration time to build, while accelerating quickly can reduce the amplitude but may leave other stresses unaddressed. In practice, operators often shift operating speed away from these resonant bands or add damping to reduce the peak response. The goal is not simply to spin faster or slower, but to find a speed range where the remaining imbalance does not excite a structural resonance.
Achieving vibration-free rotation usually requires an iterative loop between mass adjustment and speed mapping. A rotor balanced at low speed may still misbehave near its second or third critical, so field balancing at operating speed becomes necessary for high-precision equipment. Adding or removing weight at specific angular positions changes the force vector, while changing speed shifts the excitation frequency relative to the rotor's stiffness and damping. By recording vibration phase and amplitude across a speed sweep, technicians can separate mass-related vibration from bearing wear, misalignment, or looseness, and apply corrections that hold up across the intended operating range.
From CAD File to First Cut in Under a Week
Most shops talk about turnaround times, but few actually compress the gap between design and physical part. With a clean CAD file in hand, our process skips the usual back-and-forth. Once your model is uploaded, geometry checks and toolpath generation happen in parallel, not sequentially. That means a part drawn on Monday can be on a machine by Tuesday morning, and in your hands before the week ends.
The trick isn't just speed; it's removing the bottlenecks that normally stall prototypes. We don't wait for a batch of jobs to accumulate before setting up. Instead, your file is reviewed within hours, not days, and any potential issues—thin walls, impossible tolerances, or missing features—are flagged immediately with a suggested fix. You approve the tweak, and the first cut is scheduled. No lengthy quoting delays, no design handoffs lost in email threads.
That first cut often reveals more than any simulation. By getting metal or plastic under the spindle quickly, you can test form, fit, and even function while the idea is still fresh. Iterations become faster because the loop from change request to new part is measured in days, not weeks. Whether you're refining a bracket or validating a complex enclosure, the speed from CAD to first chip matters more than any glossy brochure claim.
Custom Profiles Without Hidden Tooling Charges
Most suppliers quietly add setup fees when you ask for a non-standard shape. We don’t. Every profile we quote is built to your dimensions, and the tooling is already accounted for in the piece price you approve. No line items for “die charges,” no re-quotes after the first sample.
That means you can prototype a one-off radius or a full production run of a custom cross-section without worrying about whether the math will change later. If we can extrude it, we’ll show you the exact cost before you commit. If we can’t hit the tolerance you need, we’ll tell you that upfront too.
It keeps budgets predictable and lets your design team explore options that would normally get shelved over hidden fees. You pay for material, labor, and finishing—not for the privilege of asking for something different.
Field-Simulated Wear Tests Before Your Die Ships
Every die we build goes through a wear cycle that copies the exact material, feed rate, lubrication type, and press tonnage from your production line. We run enough strokes to push the tool into its steady-state wear zone, not just a few dozen test hits. That reveals edge rounding, galling tendencies, and surface fatigue before the die ever reaches your dock.
When we spot uneven contact or early abrasion, we rework the affected areas immediately—adjusting clearances, re-polishing critical radii, or changing the coating. The result is a die that has already proven itself under field-like stress, so your first production run starts with predictable tool life instead of surprises.
FAQ
It manufactures the rotary cutting dies and supporting machinery used to shape and cut corrugated board into packaging components, focusing on tools that rotate at high speed to score, slit, and perforate material in continuous runs.
Precision engineering controls factors like runout, bearing alignment, and blade geometry. Tight tolerances reduce uneven wear and vibration, which means dies stay sharp longer and require less frequent replacement or adjustment.
Because the cylinders rotate at significant speeds, even small mass imbalances create vibrations that degrade cut quality and stress the machine frame. Proper dynamic balancing keeps the die stable during operation, protecting both the tool and the corrugated board.
Many shops start with alloy tool steels or high-speed steel for the cutting edges, while die bodies may use hardened steel or lightweight aluminum alloys. Material choice depends on run length, board thickness, and the detail level of the cutting pattern.
They rely on CNC grinding, wire EDM, and coordinate measuring machines. In-process inspection checks critical dimensions at multiple stages, and controlled temperature environments prevent thermal expansion from skewing measurements.
Polishing or coating the die surface reduces friction and adhesive buildup from corrugated board coatings. A consistent finish also ensures clean ejection of cut pieces and helps prevent premature edge chipping.
Yes. Many factories take CAD files from packaging designers and adapt the die layout, scoring rules, and perforation patterns to match specific flute profiles or folding requirements, often prototyping in-house before full production.
Conclusion
The steel in a corrugated rotary die rarely gets the attention it deserves, but it decides how long an edge stays sharp past the expected run. We select high-alloy grades for controlled carbide distribution, so blades hold their geometry through longer production windows without frequent resharpening. That durability pairs with micron-level tolerances across the cutting profile. When the die meets the anvil, a deviation of just a few microns shows up as chatter and a rougher cut. By grinding and lapping each blade to a quieter shear, we make the difference audible on the first rotation.
Precision is also about motion. A rotary die spinning at full speed has to balance mass and speed, or vibration will eat into the cutting edges and the press bearings. We dynamically balance every cylinder assembly to remove that wobble before it reaches your floor. The same urgency carries into our lead times: a CAD file becomes a first cut in under a week, and custom profiles are quoted without hidden tooling charges. Before shipping, each die goes through a field-simulated wear test that replicates your material, pressure, and duty cycle, so install day feels routine instead of experimental.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com